

A copper part can meet its conductivity target on paper and still arrive with heavy burrs, smeared edges, and a price well above the first estimate. Much of that gap starts with the grade written on the drawing, before any tool touches the bar.
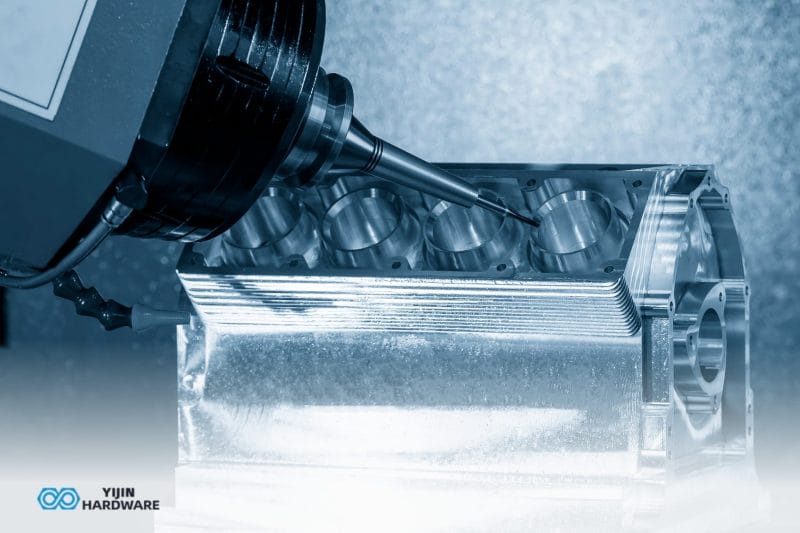
Copper CNC machining is the subtractive process of milling, turning, and drilling copper bar or plate into finished parts such as busbars, heat sinks, electrodes, and connector pins.
Each grade trades electrical conductivity against machinability, so the alloy on the drawing sets tool wear, burr size, edge quality, and cycle time. Matching the grade to the conductivity the part actually needs is the most direct route to clean edges, stable tolerances, and a predictable price per part.
Why Do Engineers Specify Machined Copper?
Copper earns its place on a drawing when a part has to carry current or heat with minimal loss. Annealed copper is defined as 100% on the International Annealed Copper Standard, or IACS, and silver is the only common metal that conducts better. That conductivity is the main reason copper machining appears on electrical and thermal drawings.
Copper’s thermal conductivity is second only to silver among common engineering metals. Copper heat spreaders and cold plates therefore hold electronics at a lower temperature, which can extend component life.
Copper also solders and brazes readily. Cold plate channels can be brazed shut instead of gasketed, and busbar joints can be brazed instead of bolted, which removes parts and assembly steps.
Machining suits copper parts that combine pockets, counterbores, and threaded mounts in one piece. Extrusion and stamping struggle to produce that mix economically. Machining also fits prototype and low-volume runs that do not justify the cost of forming tools.
Which Grades Suit Copper CNC Machining?
Copper grades fall into two groups: high-conductivity coppers and alloyed coppers that trade some conductivity for cleaner cutting or higher strength. The table below compares the grades specified most for machined parts.
| Grado | Tipo | Conductivity, % IACS | Machinability rating |
|---|---|---|---|
| C10100 | Oxygen-free electronic | 101 | 20 |
| C10200 | Oxygen-free | 101 | 20 |
| C11000 | Electrolytic tough pitch, ETP | 101 | 20 |
| C14500 | Tellurium copper | 93 | 85 |
| C18200 | Chromium copper, aged | 80 | 20 |
| C17200 | Beryllium copper, aged | 22 | 20 |
| C36000, reference | Free-cutting brass | 26 | 100 |
Machinability ratings are relative to C36000 free-cutting brass at 100, per the Copper Development Association. Conductivity values are nominal at room temperature.
Four requirements narrow the shortlist: the conductivity floor, the joining method, production volume, and strength in service. Each grade below answers one of them.
- Conductivity first: C11000 ETP copper is the default grade when conductivity matters and the part will not be brazed in a hydrogen-bearing or reducing atmosphere.
- Furnace-brazed or welded parts: C10100 and C10200 oxygen-free coppers avoid the hydrogen embrittlement that the oxygen in ETP copper can cause in a reducing atmosphere or during welding.
- High-volume turned parts: C14500 tellurium copper machining is the usual route for high-conductivity parts made in volume.
- Heat under load: C18200 chromium copper holds its strength at elevated temperatures.
- Spring force: C17200 beryllium copper applies when spring strength and fatigue life outrank conductivity.
How Does Each Copper Grade Machine?
The machinability ratings in the grade table explain most of the cycle time gap in copper machining. A low-rated grade can take several times longer to cut cleanly than a free-cutting one, depending on the feature and the finish callout.
High-conductivity coppers
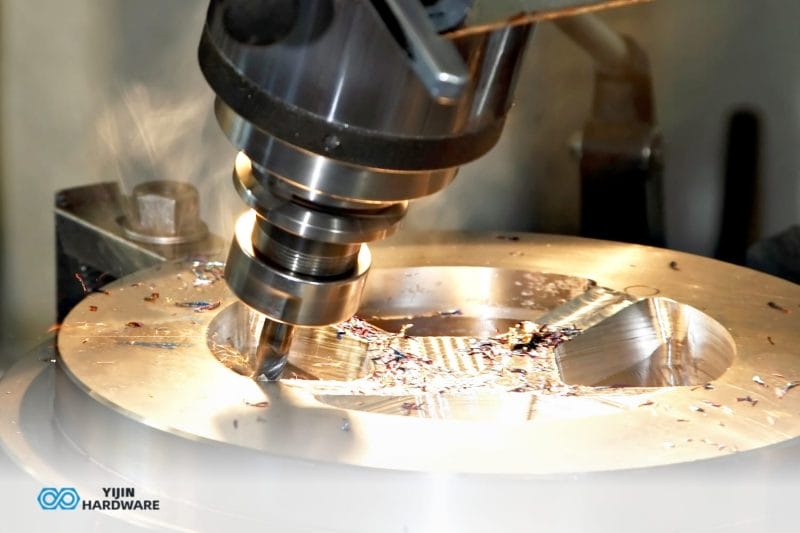
C10100, C10200, and C11000 are soft and ductile, so chips stay long and gummy and material welds onto the tool edge. That built-up edge leaves raised burrs on exit edges.
Sharp, polished, high-rake carbide tooling and flood coolant limit the buildup and keep the finish consistent. Half-hard bar, when the part allows it, smears less than annealed stock and leaves smaller burrs.
C14500 tellurium copper
Tellurium forms fine copper telluride particles that break chips short, trading a few points of conductivity for much freer cutting. On a lathe, C14500 behaves close to free-cutting brass, so cycle time drops sharply on turned pins and contacts.
Chromium copper
C18200 in the aged condition cuts more cleanly than annealed pure copper. The alloy is harder than ETP copper, so tool wear rises slightly while burrs shrink.
Beryllium copper machining
Machining C17200 starts with the temper since the alloy can be cut solution-annealed or aged. Parts cut annealed are age-hardened afterward, which raises strength and shrinks linear dimensions by about 0.2%. Tight features are often finished after aging, so the temper at machining belongs on the drawing.
Beryllium dust and fines from either temper need controlled machining practices. The US Occupational Safety and Health Administration publishes general beryllium guidance.
How Should Machined Copper Parts Be Designed?
Copper is soft, ductile, and expands more with heat than steel. Features that pass unnoticed in steel can add hours when machining copper. Four areas carry most of the cost and quality impact.
Edge breaks and burr control
An edge break called out on the drawing cuts hand deburring time and keeps edges consistent across a lot. A small chamfer or radius on exit edges covers most copper parts.
Marking which edges are cosmetic and which are functional keeps deburring tools away from contact faces. Those faces carry current, so flatness and finish matter more there than appearance.
Tool wear shows up first as burr height, since a dulled edge smears copper instead of shearing it. Internal corner radii sized for a larger, stiffer cutter slow that wear and hold burr height steady between tool changes.
Wall thickness and workholding
Thin copper walls deflect under clamping and cutting pressure, so the practical minimum depends on grade, wall height, and feature size. Aged grades and hard-temper C14500 typically hold thinner walls than annealed C11000 at the same height because their higher yield strength resists clamping distortion.
Soft jaws, sacrificial support, and lighter finishing passes keep thin sections flat. Each adds setup time, so thicker walls with no functional cost lower the price per part.
Tolerances and thermal growth
Naming ISO 2768 on the drawing covers general tolerances. Tight bands then stay on the features that need them, such as contact faces and mating bores.
Solución Yijin reviews copper drawings against ISO 2768 at the quoting stage and flags tolerances that add cycle time without a functional need.
Copper expands about 17 µm per meter for each degree Celsius. A 300 mm busbar grows roughly 0.05 mm across a 10°C swing. Long parts with tight bands need an inspection temperature on the drawing, commonly 20°C, so that supplier and customer measurements agree.
Threads and tapped holes
Soft copper threads wear quickly under repeated assembly, so thread inserts suit fasteners that come out often. In pure grades, thread forming or single-point threading often gives cleaner flanks than cut taps. Form taps need a larger pilot hole, so a drawing that states the thread class rather than a drill size leaves the shop free to choose.
Which Surface Finishes Suit Copper Parts?
Bare copper starts to tarnish soon after machining, so finish choice depends partly on how long parts sit before assembly. Many copper parts run bare, and a finish earns its place when contact, solder, or appearance requirements call for one.
| Acabado | Qué hace | Uso típico | What to state on the drawing |
|---|---|---|---|
| Cleaned, no coating | Keeps full surface conductivity | Internal busbars, EDM electrodes | Cleaning method, non-staining coolant, and sealed packaging |
| Niquelado | Barrier against corrosion and wear | Busbar terminals, connector bodies | Thickness range and masked areas |
| Silver plating | Lowest contact resistance | High-current contacts | Thickness range, tarnish protection |
| Tin plating | Solderability and low-cost protection | Terminals and lugs | Bright or matte, thickness range |
| Anti-tarnish coating or lacquer | Slows oxidation, keeps copper color | Visible parts | Masks on any contact surface |
Coatings that add contact resistance stay off contact faces through masking. Plating also adds thickness, so tight dimensions need a note stating whether they apply before or after plating.
What Copper Parts are Commonly CNC Machined?
Six part families appear often on copper drawings, from busbars to EDM electrodes. The table maps each family to the grades usually quoted for it.
| Pieza | Grade usually quoted | What drives the choice |
|---|---|---|
| Busbars and terminal blocks | C11000, C10200 | Current capacity and joining method |
| Heat sinks and cold plates | C11000, C10100, C10200 | Heat spreading across fins or channels |
| EDM electrodes | C11000, C14500 | Edge detail and electrode wear |
| Connector pins and contacts | C14500 | Conductivity at high turning volume |
| Resistance welding tips | C18200 | Hardness held at welding heat |
| Spring contacts | C17200 | Strength and fatigue life |
When Does Brass or Bronze Suit Better?
Machining copper is worth the cycle time only when the part needs the conductivity. For parts with no conductivity target, brass usually delivers the function at a shorter cycle time, and bronze adds wear resistance.
Brass suits fittings, housings, and threaded parts, and the brass CNC machining guide covers its grades and process. For parts that could go either way, the latón frente a cobre comparison sets them side by side.
Bronze suits bearings, bushings, and sliding surfaces that pure copper would gall or wear through. The bronze vs. copper comparison covers that trade-off in detail.
Specifying a Copper Grade for Machining
Copper grade selection rests on how much conductivity the part needs and how much extra machining time that conductivity is worth. Yijin Solution machines copper parts in grades including C11000, C10100, and C14500 to customer drawings, from prototypes to production lots. Engineers specifying busbars, heat sinks, or electrodes can enviar sus planos for a grade and manufacturability review.
Copper CNC Machining Guide FAQs
How much does copper CNC machining cost?
Copper CNC machining cost depends on four drivers: grade price, cycle time, tool wear, and order quantity. Alloyed grades such as C17200 carry a much higher bar price than C11000, and that gap grows on parts with heavy stock removal. Larger quantities spread setup and programming time across more parts.
Is copper or aluminum better for machined heat sinks?
Copper conducts heat at about 390 W/m·K, more than twice the rate of Aluminum 6061. It also weighs about three times as much. Copper suits compact, high-heat-flux parts, and aluminum suits weight-limited or cost-led parts.
Can copper be anodized?
Copper is not anodized the way aluminum is because its oxide does not grow into a stable protective film. Plating or a clear anti-tarnish coating provides that protection instead.
What files are needed to quote a copper part?
A copper part quote needs a 3D model, such as a STEP file, plus a 2D drawing that states grade, temper, tolerances, and finish. Quantity, inspection report needs, and any material certificate or % IACS conductivity check complete the request.
Volver arriba: Copper CNC Machining Guide: Grade Selection, Machinability and Design


Gavin Yi
Gavin Yi es un destacado líder en fabricación de precisión y tecnología CNC. Como colaborador habitual de las revistas Modern Machine Shop y American Machinist, comparte sus conocimientos sobre procesos de mecanizado avanzados e integración de Industria 4.0. Sus investigaciones sobre optimización de procesos se han publicado en Journal of Manufacturing Science and Engineering e International Journal of Machine Tools and Manufacture.
Gavin forma parte de la junta de la National Tooling & Machining Association (NTMA) y con frecuencia realiza presentaciones en la International Manufacturing Technology Show (IMTS). Cuenta con certificaciones de las principales instituciones de formación en CNC, incluido el programa de fabricación avanzada de la Goodwin University. Bajo su dirección, Shenzhen Yijin Solution colabora con DMG Mori y Haas Automation para impulsar la innovación en la fabricación de precisión.


 English
 Spanish
 German
 French